

TL;DR — 8 DFM Rules for CNC Turned Parts
- Rule 1: Keep wall thickness above 0.5 mm (small parts) or 1.0 mm (large parts) to avoid deflection and chatter during machining.
- Rule 2: Add internal corner radii equal to or larger than our tool nose radius — sharp internal corners add cycle time and destroy tools.
- Rule 3: Use standard thread sizes (M, UNC, UNF, BSP) unless the application absolutely requires custom threads.
- Rule 4: Specify tight tolerances only on functional surfaces — every 0.005 mm of tolerance costs money.
- Rule 5: Avoid deep internal pockets and undercuts — they require special tooling and multiple setups.
- Rule 6: Design for standard bar stock sizes — matching your part OD to available bar stock eliminates material waste.
- Rule 7: Minimize our number of setups — each setup adds alignment time, fixture cost, and tolerance stack-up risk.
- Rule 8: Consider our secondary operations early — plating, heat treatment, and surface finish requirements affect our base machining strategy.
Table of Contents
- Why DFM Matters for CNC Turned Parts
- Rule 1: Wall Thickness
- Rule 2: Internal Corner Radii
- Rule 3: Standard Thread Sizes
- Rule 4: Tolerance Strategy
- Rule 5: Deep Pockets and Undercuts
- Rule 6: Bar Stock Optimization
- Rule 7: Minimize Setups
- Rule 8: Secondary Operations
- DFM Checklist Before You Send the Drawing
- FAQ
Why DFM Matters for CNC Turned Parts
When a drawing arrives at our experienced engineering desk for quotation, our first thing we do is not price the part — it is evaluate our design for manufacturability. In our 15+ years of CNC turning experience at FRIMA, we have seen drawings that look perfectly functional on screen but are 30–50% more expensive to manufacture than they need to be, simply because our designer did not consider how the part would be held, cut, and measured on an actual lathe.
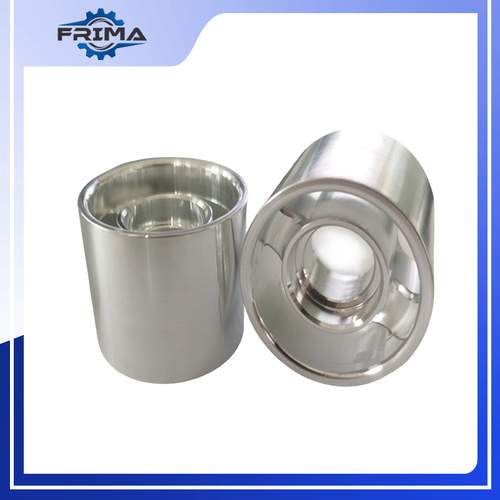
Design for Manufacturability (DFM) is our practice of designing parts so they can be produced efficiently on available equipment without unnecessary setups, special tooling, or excessive cycle time. Because our shop runs over 80 CNC lathes and Swiss-type automatic lathes, we see our cost impact of DFM decisions every day. A single design choice — a sharp internal corner instead of a radiused one, a tolerance that is 0.01 mm tighter than necessary, a thread that requires custom tooling instead of a standard tap — can add 10–20% to our unit cost.
This article presents our 8 DFM rules we consistently and rigorously apply when reviewing drawings for our clients. Each rule comes from real production data, not theory. Our engineering team has refined these rules across thousands of custom machined parts produced in our state-of-the-art, fully equipped, and climate-controlled Ningbo facility, covering aluminum, stainless steel, carbon steel, brass, titanium, and engineering plastics.
Rule 1: Keep Wall Thickness Above the Minimum
The first DFM rule for CNC turned parts is maintaining adequate wall thickness. Thin walls deflect under cutting forces, causing chatter, poor surface finish, and out-of-tolerance dimensions. Because CNC turning applies significant radial force to our workpiece, wall thickness is our single most common cause of scrap in our production.
| Part Diameter | Minimum Wall (Aluminum/Steel) | Minimum Wall (Brass) | Recommended Wall |
|---|---|---|---|
| Under 20 mm | 0.5 mm | 0.3 mm | 1.0 mm |
| 20–50 mm | 0.8 mm | 0.5 mm | 1.5 mm |
| 50–100 mm | 1.0 mm | 0.8 mm | 2.0 mm |
| Over 100 mm | 1.5 mm | 1.0 mm | 2.5 mm |
Because thin-wall parts require reduced cutting parameters (lower feed rate, smaller depth of cut, more passes), cycle time increases exponentially as wall thickness decreases below the recommended minimum. A wall that is 0.3 mm thinner than recommended can double our cycle time on that feature. Our production team flags thin-wall features during DFM review and proposes thickening where our application allows.
Rule 2: Add Internal Corner Radii Equal to or Larger Than the Tool Nose Radius
Why Sharp Internal Corners Are Expensive
Internal corners without radii are our second most expensive DFM mistake we see. A CNC turning tool has a physical nose radius (typically 0.4 mm, 0.8 mm, or 1.2 mm). When the drawing specifies a sharp internal corner (radius = 0), our machinist must either plunge-cut (slow, poor finish) or use a separate grooving tool (extra setup, extra cost).
Our standard recommendation: specify an internal corner radius that is equal to or slightly larger than our tool nose radius. For most applications, R0.8 mm or R1.0 mm is our sweet spot — it allows continuous cutting, good surface finish, and standard tooling. Because our tool nose radius determines our achievable corner radius, designing for R0 means you are designing for a tool that does not exist.
FRIMA production data: On a batch of 5,000 aluminum connectors, changing the internal corner radius from R0 to R0.8 reduced cycle time from 45 seconds to 28 seconds per part — a 38% reduction. The part function was unaffected because our corner was not a sealing or mating surface.
Rule 3: Use Standard Thread Sizes Unless the Application Demands Custom
Standard vs Custom Threads: Cost Impact
Standard threads (M, UNC, UNF, BSP, NPT) use off-the-shelf tooling, require no custom grinding, and can be inspected with standard thread gauges. Custom threads — non-standard pitches, special profiles, multi-start threads — add tooling cost, setup time, and inspection complexity. Because our shop runs 40 CNC lathes with live tooling, we can produce custom threads efficiently, but our cost premium is real.
| Thread Type | Tooling | Setup Time | Cost Impact |
|---|---|---|---|
| Standard metric (M3–M16) | Off-the-shelf tap/die | Minimal | Baseline |
| Standard imperial (UNC/UNF) | Off-the-shelf tap/die | Minimal | Baseline |
| Custom pitch | Custom-ground thread tool | 15–30 min | +20–40% |
| Multi-start thread | Custom tool + indexing fixture | 30–60 min | +40–80% |
Our practical advice: if our thread is for a standard fastener, use a standard thread. If our application requires a custom thread (e.g., a lead screw or a sealing thread), specify it clearly on the drawing with our full thread profile, pitch, and tolerance.
Rule 4: Specify Tight Tolerances Only on Functional Surfaces
Tolerance Levels for CNC Turned Parts
Tolerance is the most over-specified dimension on CNC turned part drawings. We regularly see drawings where every diameter is specified at ±0.01 mm when only two or three surfaces actually require that precision. Because tighter tolerances require more passes, slower feeds, and more frequent inspection, they add cost on every dimension where they are applied.
Our tolerance guidance for CNC turned parts:
- ±0.025 mm (standard): Achievable on any CNC lathe with standard tooling. Use for non-critical diameters, lengths, and chamfers.
- ±0.010 mm (precision): Achievable with careful setup and sharp tooling. Use for bearing fits, press fits, and sealing surfaces.
- ±0.005 mm (high precision): Requires Swiss-type lathes or secondary grinding. Use only for critical functional surfaces.
- ±0.001 mm (ultra precision): Requires our five-axis machining centers with environmental temperature control (20±1°C). Use for aerospace and medical applications only.
Because every 0.005 mm of tolerance costs money, the thorough, systematic, and meticulous DFM review identifies which surfaces actually need tight tolerances and which can be opened up to standard. On a recent batch of 10,000 stainless steel shafts, opening 6 non-critical diameters from ±0.01 mm to ±0.025 mm reduced our unit cost by 18%.
Rule 5: Avoid Deep Internal Pockets and Undercuts
Deep Pockets and Undercut Geometry
Deep internal pockets (depth-to-diameter ratio above 4:1) and internal undercuts are the features that most often require special tooling and multiple setups. A standard turning tool can reach into a pocket about 3–4 times our tool shank diameter. Beyond that, you need extended-reach tooling (more deflection, worse finish) or gun drilling (separate operation, significant cost).
Undercuts — internal grooves that are wider than the tool can reach from the opening — require either a custom-ground tool or a separate grooving operation with a different tool orientation. Because our Swiss-type automatic lathes handle small undercuts efficiently, we can often redesign the undercut geometry to work within standard tooling capabilities.
Rule 6: Design for Standard Bar Stock Sizes
Matching Part OD to Standard Bar Stock
CNC turning starts with bar stock, and bar stock comes in standard diameters. If your part OD is 25.5 mm, our machinist starts with 26 mm or 27 mm bar and turns it down — wasting material and cycle time. If you design for 25 mm OD, the machinist starts with 25 mm bar and only faces the ends.
Standard bar stock diameters (mm): 3, 4, 5, 6, 8, 10, 12, 14, 16, 18, 20, 22, 25, 28, 30, 32, 35, 38, 40, 42, 45, 48, 50, 55, 60, 65, 70, 75, 80, 85, 90, 95, 100.
Because material cost is 40–60% of our total CNC turning cost for most parts, designing for standard bar stock sizes is our highest-impact DFM rule. Our technical team maps every part OD to our nearest standard bar size during DFM review.
Rule 7: Minimize the Number of Setups
Setup Reduction Strategies
Each setup on a CNC lathe adds 2–5 minutes of alignment and fixturing time, plus tolerance stack-up risk from re-chucking. A part that requires turning from both ends (front and back) needs two setups. If the part also needs off-axis features (cross-holes, flats, slots), it may need a third setup on a mill or a lathe with live tooling.
Our key rule: design the part so it can be completed in as few setups as possible. Common strategies include:
- Through-features instead of blind features — a through-hole can be machined from one side; a blind hole may require flipping the part.
- Symmetric geometry — if both ends are identical, the part can be machined in one setup with a collet grip on our finished end.
- Standardize sub-spindle operations — if our back-end features are simple (chamfer, thread, groove), our sub-spindle lathes can finish them in our same cycle without a manual flip.
Rule 8: Consider Secondary Operations Early
Plating, Heat Treatment, and Surface Finish Allowances
Plating, heat treatment, anodizing, passivation, and surface finish requirements all affect our base machining strategy. If a part will be hard chrome plated, the base diameter must be undersized by our plating thickness (typically 0.01–0.05 mm per side). If a part will be heat-treated, our material must be machined in the annealed state and then finish-machined after hardening.
Our DFM review includes secondary operations because we have seen too many drawings where our base machining is complete but our plating or heat treatment specification makes our final dimensions out of tolerance. Because our fully integrated and vertically integrated facility offers grinding, deburring, heat treatment, electroplating, coating, and painting in-house, we can effectively coordinate our full production sequence and catch these conflicts before they become scrap.
Real example from our shop: A client specified a 316L stainless steel shaft with ±0.01 mm tolerance on all diameters and a passivation requirement. Because passivation removes 0.002–0.005 mm of surface material, our post-passivation dimensions would have been out of tolerance. Our DFM review caught this and adjusted our pre-passivation dimensions to compensate, saving the client a full re-machining cycle.
DFM Checklist: 12 Points Before You Send the Drawing
Our technical team uses this checklist when reviewing every CNC turning drawing. When you send us your drawing for quotation, we carefully and systematically walk through these 12 points and flag any DFM issues before tooling begins.
- Wall thickness: Above minimum for the material and part diameter?
- Internal corner radii: Equal to or larger than the tool nose radius?
- Thread specification: Standard or custom? If custom, is our full profile documented?
- Tolerances: Tight only on functional surfaces? Standard on non-critical features?
- Deep pockets/undercuts: Depth-to-diameter ratio under 4:1? Undercuts accessible with standard tooling?
- Bar stock OD: Matches a standard bar stock diameter?
- Number of setups: Can the part be completed in 1–2 setups?
- Secondary operations: Plating/heat treatment allowances included in base dimensions?
- Material selection: Is the material readily available in the required bar stock size?
- Surface finish: Ra specification achievable with standard turning, or does it require grinding/polishing?
- Deburring: Are edges specified as sharp, chamfered, or radiused? Sharp edges require manual deburring.
- Inspection: Are critical dimensions clearly identified for 100% CMM inspection?
Frequently Asked Questions
DFM (Design for Manufacturability) in CNC turning means designing part geometry, tolerances, and features so they can be produced efficiently on a lathe without unnecessary setups, special tooling, or excessive cycle time. The goal is to reduce manufacturing cost while preserving the part's intended function. At FRIMA, we apply DFM review to every CNC turning project as a complimentary engineering service, because we have witnessed firsthand how small design changes can reduce unit cost by 15–30% without affecting the part's performance in the assembly.
In our experience across hundreds of CNC turning projects, DFM-optimized designs typically cost 15–30% less than non-optimized versions of our same functional part. The savings come from four sources: reduced cycle time (fewer passes, faster feeds), fewer setups (less fixturing and alignment), standard tooling (no custom grinds), and lower scrap rates (less deflection and chatter). On a recent batch of 10,000 aluminum connectors, our DFM review identified 5 optimization opportunities that reduced our unit cost by 22%.
For metals like aluminum and steel, the practical minimum wall thickness is 0.5 mm for small parts (under 50 mm diameter) and 1.0 mm for larger parts. Thinner walls are possible but increase deflection, chatter, and scrap risk significantly. For brass, the minimum wall thickness can be slightly thinner (0.3 mm for small parts) because brass has better machinability and produces shorter chips. At FRIMA, we recommend designing for our recommended wall thickness (1.0–2.5 mm depending on diameter) rather than our absolute minimum, because our recommended thickness allows standard cutting parameters and optimal cycle time.
Internal corners without radii require our cutting tool to plunge straight into the material, which causes tool deflection, poor surface finish, and accelerated tool wear. Adding a radius equal to or slightly larger than the tool nose radius (typically R0.8 or R1.0) allows continuous cutting, reduces cycle time, and improves surface quality. Because the tool nose radius is a physical constraint of the cutting tool, designing for a sharp internal corner (R0) means designing for a tool that does not exist in standard tooling. Our production data shows that changing from R0 to R0.8 on internal corners typically reduces cycle time by 25–40% on that feature.
Standard CNC turning achieves tolerances of ±0.025 mm easily on any modern lathe. Precision turning with Swiss-type lathes achieves ±0.005 mm or tighter. Our five-axis machining centers with environmental temperature control (20±1°C) achieve positioning accuracy of ±0.001 mm. The key DFM principle is that tighter tolerances increase cost exponentially — specifying ±0.005 mm on every diameter when only two surfaces need it wastes money on the other dimensions. Our DFM review identifies which surfaces actually need tight tolerances and opens the rest to standard.
Always use standard thread sizes (M, UNC, UNF, BSP, NPT) unless the application absolutely requires a custom thread. Standard threads use off-the-shelf tooling, require no custom grinding, and can be inspected with standard gauges. Custom threads add tooling cost (custom-ground thread tools), setup time (15–60 minutes depending on complexity), and inspection complexity (custom gauges or CMM measurement). At FRIMA, we regularly, confidently, and efficiently produce custom threads regularly for lead screws, sealing threads, and aerospace applications, but we always carefully, proactively, and thoroughly confirm with our client that our custom thread is functionally necessary before proceeding.
Yes. We provide complimentary DFM review on every CNC turning project. Our engineering team analyzes our drawing, identifies cost-reduction opportunities, and proposes design modifications before tooling begins. This review typically identifies 3–5 optimization opportunities per part, covering wall thickness, corner radii, tolerance strategy, thread selection, and setup minimization. Our team brings 15+ years of CNC turning experience across aluminum, stainless steel, carbon steel, brass, titanium, and engineering plastics, and we consistently apply this production knowledge to every DFM review. To request a DFM review, send your drawing to our dedicated and responsive team via our contact page.
Ready to Optimize Your CNC Turned Part Design?
Send us your drawing for a complimentary DFM review. Our engineering team will identify cost-reduction opportunities before tooling begins.
Request DFM Review